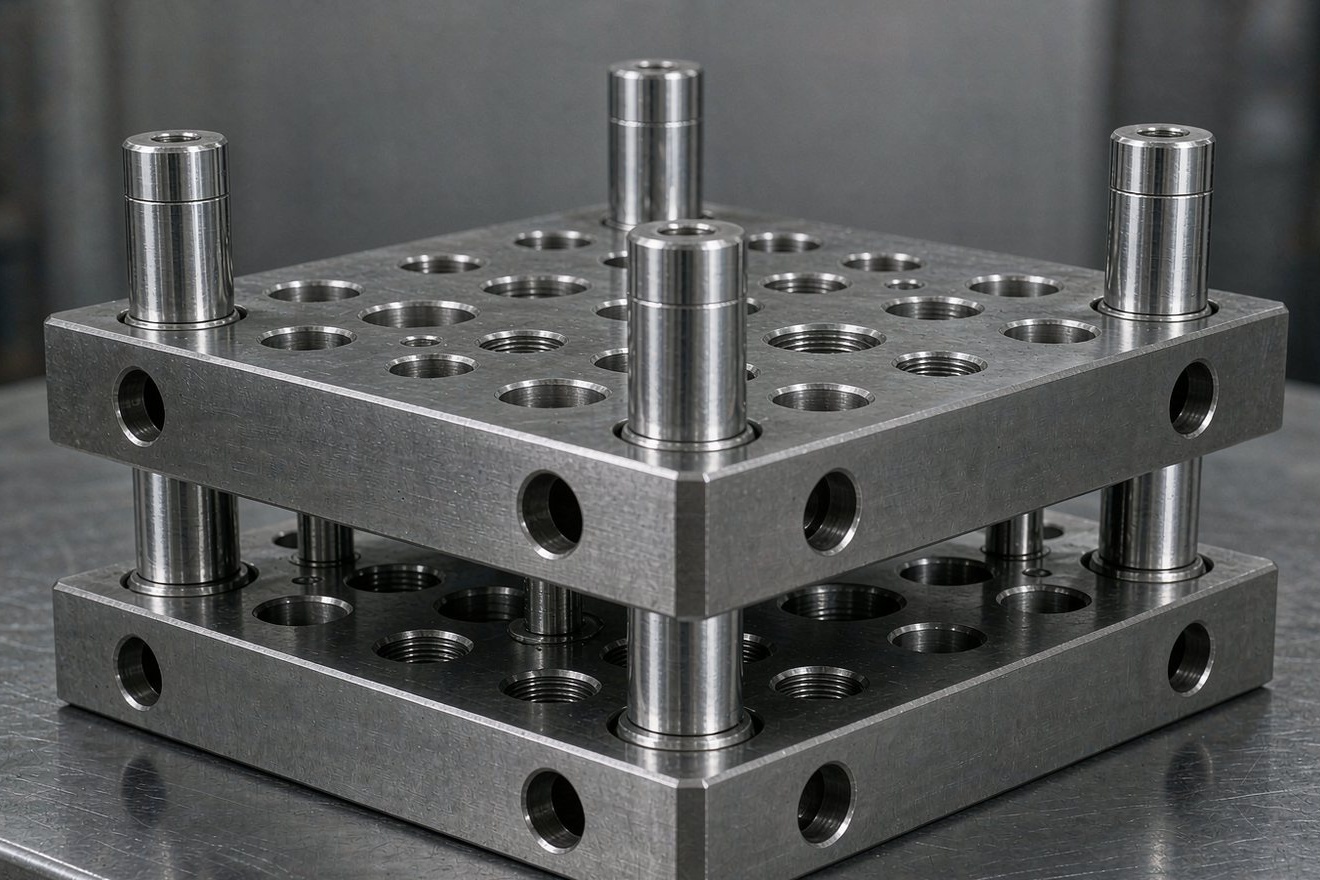
A/B/C/D plate types built to HASCO, DME and LKM systems, 1515 to 8080 mm, in 45#, S50C, P20 and 718H. Stocked plates ship in 7 days; every base leaves with CMM data for the guide-pillar bores and plate thickness.

Most standard mold base problems are dimensional: a plate that is 0.3 mm off breaks the interchangeability that makes standard bases cheap. We machine to the standard, not near it.
Two-plate design with a direct sprue gate. The workhorse for single-cavity parts and simple multi-cavity layouts.
Three-plate design for pin-point or runner systems, with a stripper plate and separate runner plate.
Three-plate structure for edge-gated parts that need the runner on the parting line, common in appliance and auto parts.
Heavy frame for large moulds: thickened clamping plates, additional support pillars, lifting provisions to your crane capacity.
S50C, 45#, P20 and 718H plates precut and pre-milled to your finished size + grinding allowance, kept in stock for repeat jobs.
Wear plates, angle pins, slide bases and insert pockets machined into the standard frame without breaking the standard envelope.
The table below is routine production capability for standard bases. If your drawing sits outside it, we say so at review instead of discovering it on the shop floor.
| Item | Range / Standard | Notes |
|---|---|---|
| Plate sizes | 1515 – 8080 mm (standard series); up to 2000 × 1300 × 800 mm for single plates | Larger frames assembled from machined sections |
| Plate thickness | 20 – 300 mm standard; up to 500 mm on request | Stress-relieved before finish machining |
| Standards | HASCO, DME, LKM (龙记), MISUMI-equivalent, or your own drawing | Interchangeability checked against the standard plate drawing |
| Steel grades | 45#, S50C, 40Cr, P20, 718H, S136, NAK80 | Mill certificate with heat number; hardness test on request |
| Machining tolerance | ±0.01 mm general; ±0.005 mm precision fits | Coordinate grinding to ±0.001 mm on guide-bush bores |
| Surface finish | Ra 0.8 – 3.2 µm on fitting faces | Ra 0.4 µm on request |
| Guide pillar bores | H7 fit, perpendicularity ≤0.01/100 mm | Measured on CMM, recorded per bore |
| Lead time | 7 days stocked plates; 12 – 20 days machined to drawing | Confirmed in writing at order, not at shipment |
| Inspection | CMM report on guide-pillar bores, plate thickness and squareness | PDF report attached to the packing list |
Values are our routine capability, not a marketing ceiling. Anything outside the range goes through a technical review first — we confirm feasibility before quoting, and we do not promise what the machines cannot hold.
Five steps, each with a named owner and a date you can hold us to. No step starts before the previous one is signed off.
We check the base against the standard plate table, flag anything that cannot be machined as drawn, and quote with the corrected dimensions listed.
24 hoursPlate is cut from certified stock, mill certificate filed against your order number, saw cut with grinding allowance.
1–3 daysRough machining, then stress relief before finishing so the plate does not move after assembly.
2–4 daysBores, pockets and faces on CNC and jig grinder; fitting faces measured in-process, not only at the end.
3–10 daysGuide-pillar bores, thickness and squareness measured and recorded; report packed with the crate; fumigated crate for sea freight.
1–2 daysStandard bases are priced from plate size, thickness, steel grade and machining scope — not from a vague "per set" rate. Give us the list and we return a line-by-line quote with the delivery date and the tolerance we will actually hold.
Straight answers to the questions buyers actually ask before the first order.
Standard work is fast when the information is complete. The list on the left is everything our estimator needs; anything missing, we will ask for once rather than guess.
Mr. Ma (马总)
Mobile / WeChat: +86 138 2921 4701
Tel: +86 769 82986196
Email: sales@layjun.cn
No. 6 Dong’ao 3rd Road, Hengli Town, Dongguan, Guangdong, China
Working hours: Mon–Sat 08:00–20:00 (GMT+8)